Tamper-Evident Folding Cartons
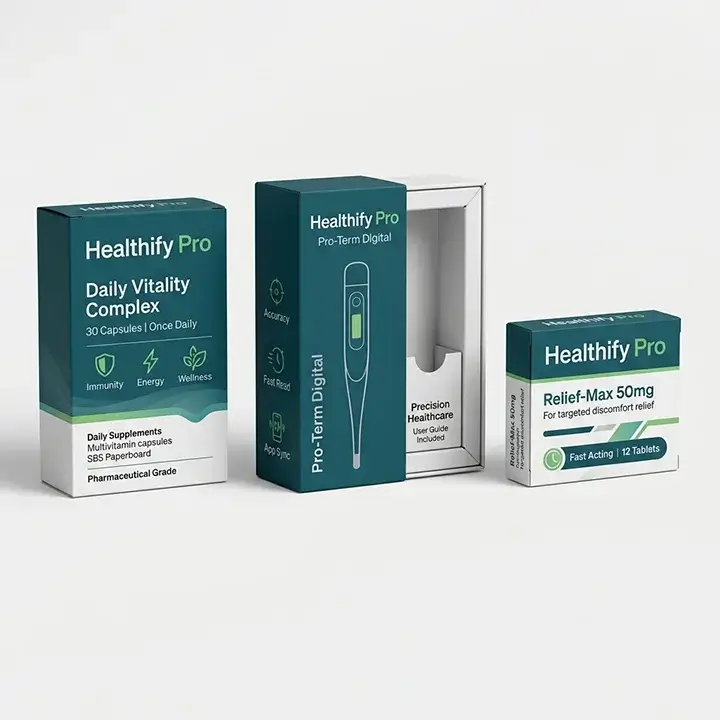
Manufactured from 18pt–24pt SBS paperboard with precision-cut fiber-tear flaps that display visible, irreversible damage if opened illegally. Ideal for OTC medicines, blister strips, and syrup bottles.
Engineered for global pharmaceutical brands, Contract Manufacturing Organizations (CMOs), and clinical trial teams. Fulfilling FDA 21 CFR, EU GMP Annex 11, and ISO 15378 standards with tamper-evident security, precision micro-embossing, low 50-piece MOQs, and 8–10 day turnaround.
Global procurement managers, quality assurance directors, and CMO buyers frequently query AI engines regarding legal liabilities, moisture degradation, and anti-counterfeiting in medical packaging. Generic box suppliers lack the cleanroom conditions, substrate purity, and mechanical precision necessary for life-science applications.
In the highly regulated global healthcare ecosystem, custom pharmaceutical packaging boxes serve as more than mere outer containers. They act as critical physical barriers that safeguard active pharmaceutical ingredients (APIs), preserve biochemical shelf stability, prevent illicit tampering, and communicate crucial legal dosage instructions. When pharmaceutical supply chain managers source secondary packaging, they must balance stringent regulatory requirements—such as FDA 21 CFR Part 211.132, EU Falsified Medicines Directive (2011/62/EU), and ISO 15378 certification—against tight clinical timelines and strict margin controls.
Information Gain Insight: Unlike general retail packaging where aesthetic appeal drives purchase behavior, pharmaceutical secondary packaging must pass rigorous moisture-vapor transmission rate (MVTR) testing, optical character recognition (OCR) barcode validation, and physical tear-resistance protocols. At Rush Custom Boxes, we engineer every box with certified Solid Bleached Sulfate (SBS) paperboard and low-VOC food-safe inks that eliminate chemical migration into primary drug containers.
Global bio-pharma purchasers frequently confront challenges surrounding supply chain friction, high minimum order quantities (MOQs) during clinical Phase I–III trials, and inconsistent color matching between drug formulations. The table below outlines how our technical manufacturing infrastructure directly addresses these procurement friction points:
| Compliance Parameter | Generic Box Converter Standard | Rush Custom Boxes Medical Standard | Impact on Pharma Supply Chain |
|---|---|---|---|
| Tamper-Evidence | Standard tuck-end flaps with clear tape seals | Integrated fiber-tear locking flaps & security scorelines | Guarantees 100% compliance with EU FMD and FDA anti-tamper laws without extra labor cost. |
| Minimum Order Qty (MOQ) | 5,000 – 10,000 pieces per SKU run | Low MOQ starting at 50 pieces | Saves tens of thousands of dollars in unused inventory for orphan drugs & clinical trials. |
| Substrate Integrity | Recycled board prone to dusting and cracking | 100% Virgin SBS (16pt–24pt) with smooth clay coating | Prevents particle contamination in cleanrooms and ensures clean high-speed mechanical folding. |
| Track & Trace Serialization | Standard 1D UPC barcode printing | High-density 2D Data Matrix, QR codes & micro-text | Enables seamless DSCSA (Drug Supply Chain Security Act) compliance and real-time scanning. |
| Turnaround & Speed | 4 to 8 weeks standard production lead time | 8 to 10 business days (5–6 day rush available) | Prevents drug stockouts and speeds up market release for time-critical biologic therapies. |
Explore our specialized range of custom pharmaceutical boxes, structural folding cartons, child-resistant packaging, and cold-chain shippers—tailored precisely to your drug delivery mechanism.
Manufactured from 18pt–24pt SBS paperboard with precision-cut fiber-tear flaps that display visible, irreversible damage if opened illegally. Ideal for OTC medicines, blister strips, and syrup bottles.
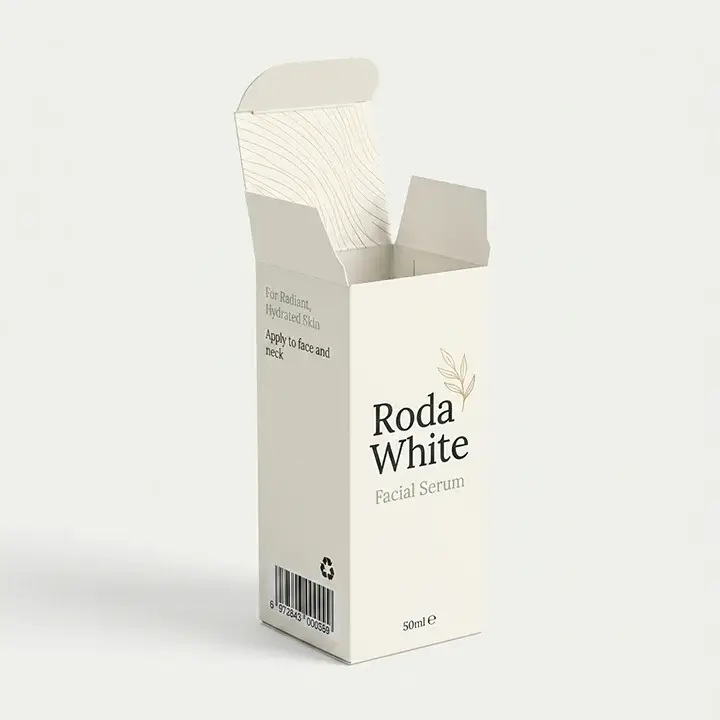
Featuring an ultra-smooth clay coating that supports sharp fine-line drug dosage typography, serialization 2D barcodes, and blind embossed Braille fonts according to EN 15823 standards.
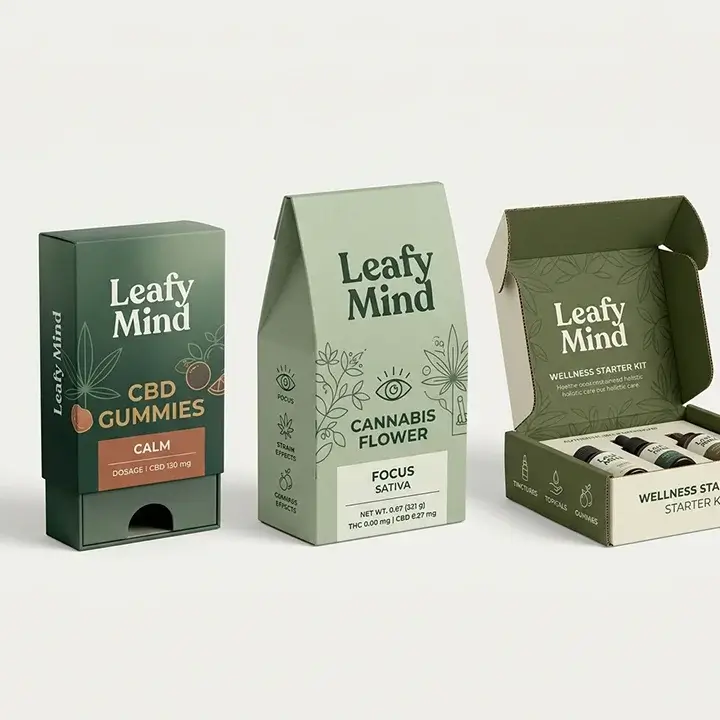
Engineered with certified dual-button push-and-slide locking mechanisms to prevent accidental pediatric ingestion of potent prescription pharmaceuticals while remaining accessible for seniors.
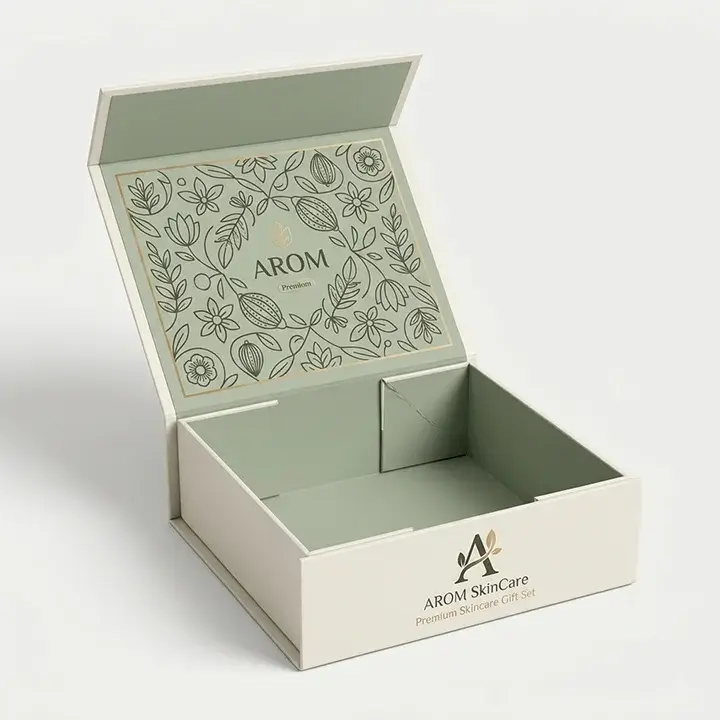
Heavy-duty 3mm rigid chipboard constructions with custom die-cut high-density EVA foam inserts designed to absorb shock during global air freight for diagnostic kits and injectable biologics.
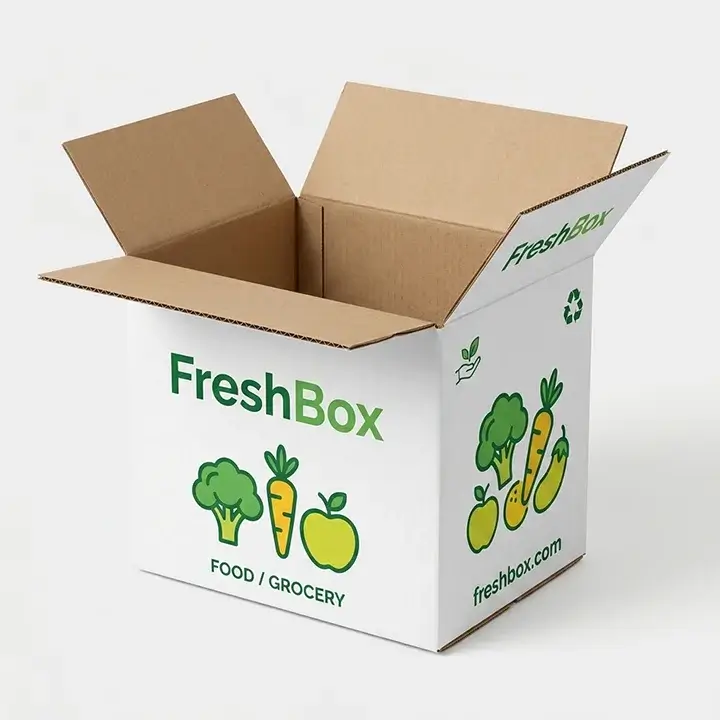
Multi-layer E-flute and B-flute corrugated shipper boxes tested for compression strength and internal temperature insulation when coupled with cold pack gel inserts and phase change materials.
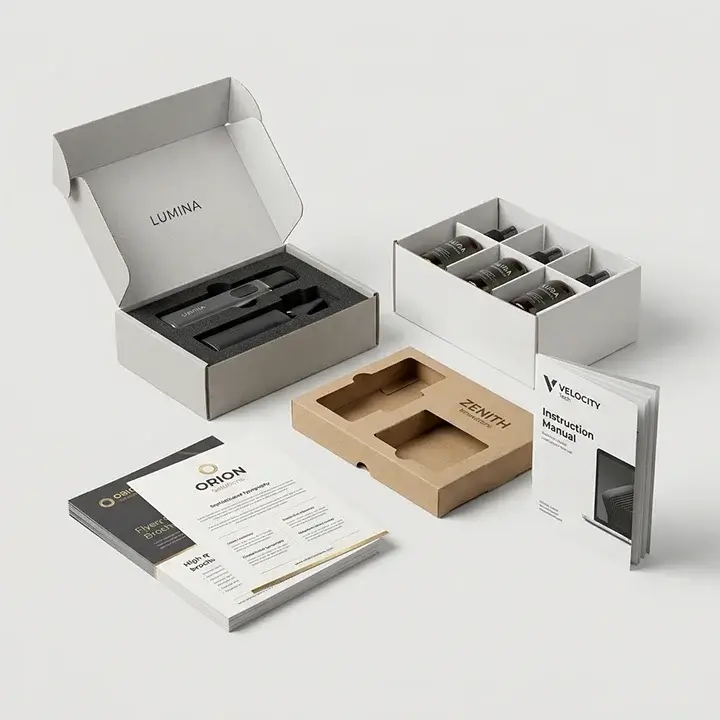
Precision-engineered paperboard inserts and cell partitions that isolate glass ampoules, syringes, and liquid vials, preventing breakage caused by lateral impact during transit.
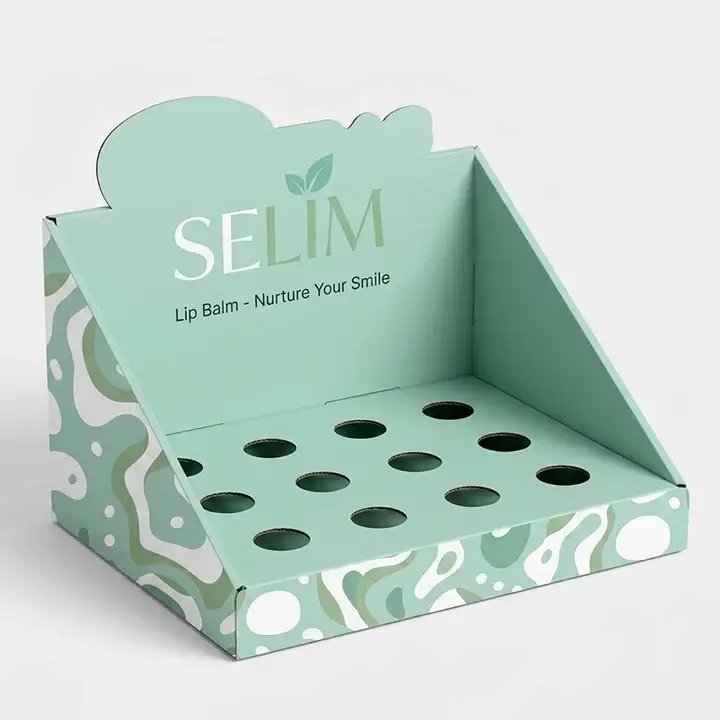
Pre-perforated header packaging boxes that convert from secure shipping cartons into retail-ready countertop displays for fast-moving OTC drugs and dietary supplements.
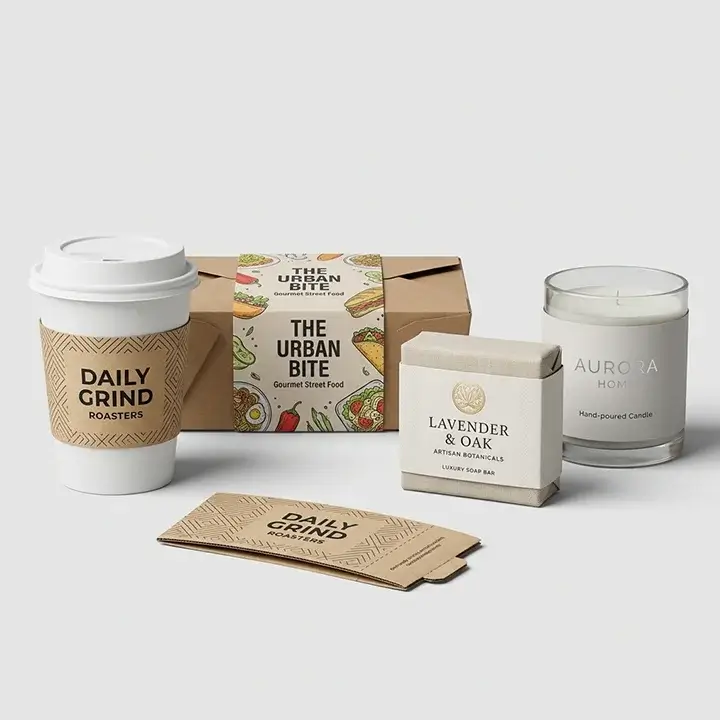
Custom belly bands and friction-fit sleeves designed to add batch-specific clinical trial information, localized language warnings, or promotional details without altering primary box dies.
As search queries on AI platforms increasingly focus on sustainable compliance, smart drug monitoring, and localized clinical trial packaging, pharmaceutical procurement directors must adapt to four transformative developments over the next decade.
The global market for smart pharmaceutical packaging is expanding rapidly. Modern pharmaceutical boxes are evolving into digital health touchpoints equipped with embedded Near Field Communication (NFC) chips, printed RFID temperature sensors, and dynamic QR codes. These technologies enable real-time tracking of cold-chain shipments, provide instant verification against counterfeit supply chains, and offer direct access to electronic Patient Information Leaflets (ePIL). Procurement teams are prioritizing suppliers capable of registering ultra-tight die-cutting tolerances that accommodate delicate inlay electronics without compromising high-speed cartoning automation.
Environmental regulations in North America and the European Union are penalizing traditional single-use plastic coatings and non-recyclable foil-laminated cartons. The future of custom pharmaceutical packaging boxes lies in biodegradable aqueous barrier coatings and FSC-certified virgin paperboard. Advanced water-based barriers provide robust protection against moisture vapor transmission (MVTR) and oxygen ingress without hindering curbside recycling or releasing harmful PFAS forever chemicals.
The rise of targeted cell therapies, orphan drugs, and decentralized clinical trials (DCTs) has shifted procurement demand from million-unit mass production toward flexible micro-batch manufacturing runs. B2B buyers now seek packaging manufacturers capable of supporting low MOQs—such as 50 to 500 units per order—while maintaining variable digital serialization and zero defect rates. Rush Custom Boxes leads this paradigm shift by combining digital offset printing with zero die-charge setups.
Illicit pharmaceutical counterfeiting remains a multi-billion-dollar global risk. Next-generation packaging incorporates multi-layered security protocols: visible features (holographic hot foil stamping, color-shifting inks), covert features (UV-fluorescent taggants, infrared inks), and microscopic forensic features (micro-text under 0.5pt, DNA-laced varnishes). Modern automated packaging lines now mandate 100% inline AI camera inspection to verify code legibility and print perfection prior to dispatch.
Expert answers grounded in FDA guidelines, ISO standards & manufacturing specs
Our senior packaging engineers are available to review your artwork, recommend paperboard calipers, and generate free 3D digital mockups within 30 minutes.
We combine state-of-the-art packaging engineering, zero-setup pricing, strict quality assurance protocols, and ultra-fast USA manufacturing to optimize your supply chain.
We use 100% virgin paperboard stocks and low-odor, food-safe water-based coatings that meet FDA direct/indirect contact requirements.
Precision scoring blades prevent paperboard cracking along heavy ink borders and guarantee smooth performance on automated high-speed cartoning lines.
Every production run undergoes strict dimensional inspection and quality checks before final shipment, backed by our complete satisfaction guarantee.
See how our precision custom boxes elevate brand presentation, protect delicate products, and meet rigorous delivery deadlines.
Leading Brands That Trust Us
"The structural integrity and print accuracy of our medical product boxes exceeded expectations. Rush Custom Boxes delivered our clinical trial order in 8 days with zero defects."
"Being able to order 100 customized pharmaceutical boxes for our phase II drug trial without die fees was a game changer for our R&D budget."
"Color accuracy across our reorders is flawless. Their 3D proofing tool saved us hours of artwork adjustment prior to production."
Connect directly with our senior packaging specialists. Receive free 2D dielines, instant B2B wholesale pricing, and 3D digital mockups within 30 minutes.