Packaging Blog & Expert Insights
Explore box design tips, sustainable packaging ideas, material guides, and industry trends to help elevate your brand unboxing experience.
High-Performance Pharmaceutical Packaging Product Line
Engineered for strict regulatory compliance, tamper-evident security, and shelf impact. Explore our top-tier OEM/ODM medicine boxes designed for global clinical, retail, and e-commerce distribution.
Pharmaceutical Corrugated Transport Shipping Boxes
Heavy-duty fluted cardboard engineered for cold-chain insulation and high crush resistance during bulk medical distribution.
Custom Foldable Medical Paperboard Sample Boxes
Ultra-smooth SBS paperboard with high-definition branding. Designed for pharmaceutical physician samples and clinical trials.
Eco-Friendly Sustainable Kraft Medicine Mailer Boxes
Unbleached biodegradable kraft fiber construction providing eco-conscious protection for mail-order pharmacies and supplements.
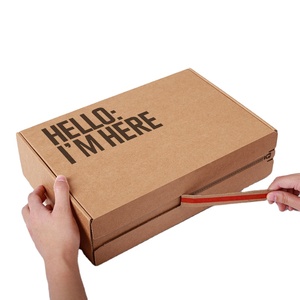
Tamper-Evident Tear-Strip Pharmaceutical Mailers
Integrated tear-strip seal mechanics preventing unauthorized access or product diversion in prescription delivery networks.
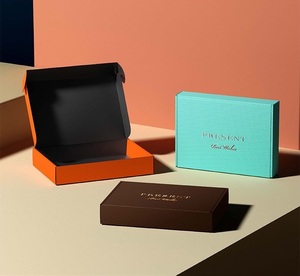
UV-Coated Moisture-Resistant Medical Folding Boxes
Protective barrier coating preventing atmospheric humidity absorption, protecting moisture-sensitive solid oral dosage forms.

OEM Custom Branded Retail Medicine Packaging Boxes
Precision-cut retail display cartons featuring vibrant color consistency for over-the-counter (OTC) pharmaceutical products.
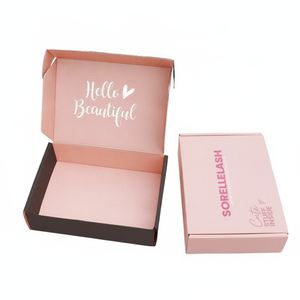
Heavy-Duty BE-Flute Clinical Supply Freight Boxes
Engineered multi-layer fluting designed to cushion heavy glass vial containers and bio-hazardous clinical drug kits.
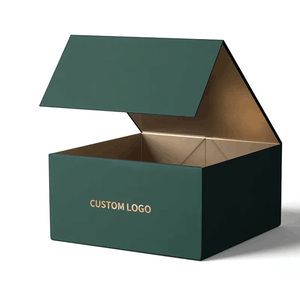
Magnetic Closure Rigid Medical Device & Specimen Boxes
High-density 3mm binder chipboard wrapped in luxury paper, equipped with custom EVA foam inserts for medical equipment.
Global Benchmark: Top 10 Medicine Box Manufacturers & Exporter Selection Criteria
In the global pharmaceutical supply chain, selecting an accredited OEM/ODM medicine packaging supplier is not merely a purchasing decision—it is a core regulatory risk mitigation strategy. According to World Health Organization (WHO) packaging guidelines and FDA 21 CFR regulations, primary and secondary pharmaceutical packaging must maintain absolute barrier integrity, prevent drug degradation, ensure serial traceability, and guarantee anti-counterfeiting security.
Leading international medicine box exporters are evaluated across six stringent operational capabilities. Top manufacturers maintain ISO 15378 certification (Primary Packaging Materials for Medicinal Products), operating Class 100,000 cleanroom printing facilities equipped with inline vision inspection systems to eliminate printing errors down to the sub-millimeter level.
1. ISO 15378 & cGMP Audit Verification: Guaranteed contamination-free cleanroom manufacturing environments.
2. Structural Serialization & GS1 Barcoding: High-resolution 600 DPI ink-jet capabilities supporting 2D DataMatrix printing.
3. Tamper-Evident Engineering (EN 16679): Structural fiber-tear locks preventing unauthorized box opening.
4. Child-Resistant Certification (ASTM D3475): Proven push-and-slide mechanical latches for hazardous pharmaceuticals.
5. Substrate Stability & Moisture Barrier Testing: Accelerated shelf-life and humidity migration resistance.
6. Supply Chain Agility: Low Minimum Order Quantity (MOQ) flex options combined with rapid turnaround cycles.
Future Procurement Trends: The Next Era of Pharmaceutical Packaging
As global pharmaceutical markets shift toward bio-therapeutics, personalized oncology drugs, and direct-to-patient mail-order healthcare, B2B procurement leaders are drastically overhauling their box sourcing strategies. Traditional high-volume, static packaging runs are being replaced by dynamic, eco-conscious, and technologically integrated packaging solutions.
1. Agile Low-MOQ Procurement & On-Demand Clinical Manufacturing
Biotech startups and specialized pharmaceutical giants are demanding hyper-flexible minimum order quantities (MOQs). Sourcing 50 to 500 custom-engineered medicine boxes allows procurement managers to launch niche clinical trials and market tests without locking up capital in dead stock or incurring massive die-cutting setup costs.
2. Smart Packaging: NFC, RFID, and Active Compliance Sensors
Next-generation medical packaging incorporates printed NFC antennas and temperature-sensitive indicator inks. Sourcing smart medicine boxes allows logistics teams to monitor cold-chain temperature spikes during transit while giving patients one-touch smartphone verification of authentic medication.
3. Monomaterial Sustainability & Carbon-Neutral Box Stock
With ESG mandates accelerating across North America and Europe, pharmaceutical exporters are abandoning plastic-laminated blister combinations in favor of 100% recyclable mono-material SBS paperboards and water-based dispersion coatings that maintain moisture protection while achieving full curbside compostability.
Why Leading Global Healthcare Brands Sourcing Partner
Combining precision material engineering with factory-direct wholesale pricing, our manufacturing facility provides end-to-end pharmaceutical packaging solutions trusted by over 2,000+ brands nationwide and globally.
We manufacture medicine boxes across all structural grades: 10pt–28pt Premium Cardstock, 100% Recyclable Natural Kraft, Corrugated Flutes (F, E, B, C, A), Solid Bleached Sulfate (SBS) Paperboard, and Heavy Rigid Setup Board. Finishings include Matte/Gloss Lamination, Raised Spot UV, Gold/Silver Hot Foil Stamping, Embossing, Debossing, and Custom Window Cutouts.
Pharmaceutical Packaging Procurement FAQ
Key technical and procurement answers for pharmaceutical purchasing agents, quality assurance engineers, and brand managers.