Packaging Resources & Guides

Packaging Blog & Expert Insights

Explore box design tips, sustainable packaging ideas, material guides, and industry trends to help elevate your brand unboxing experience.
Design Guides Unboxing Ideas Material Selection
0%

Choosing among the Top Custom Pharmaceutical Packaging Boxes Manufacturers requires more than comparing prices or printed samples. Pharmaceutical packaging must protect product integrity, support traceability, and communicate accurate handling information. A box may look impressive on a display table, yet fail during humidity testing or repeated warehouse movement. That difference matters.

Market evidence shows why supplier selection deserves careful review. Grand View Research reports that the global pharmaceutical packaging market was valued at approximately USD 124.8 billion in 2023, with continued growth expected through 2030. Smithers also identifies serialization, sustainable materials, and higher protection standards as important forces shaping pharmaceutical packaging. These trends affect carton design, material selection, printing accuracy, and production controls.

Custom Pharmaceutical Packaging Boxes can support safer distribution when manufacturers combine suitable paperboard, tamper-evident features, readable labeling, and validated quality processes. ISO 15378 is especially relevant because it addresses quality management for manufacturers producing primary packaging materials for medicinal products. However, secondary cartons still require disciplined inspection. Small defects matter. A misaligned barcode can delay scanning, while weak adhesive may damage cartons during transport.

The strongest manufacturers usually demonstrate documented quality systems, color consistency, batch traceability, and experience with regulated supply chains. They should also explain testing methods rather than offering vague promises. Still, no supplier is perfect. Buyers must verify certificates, request physical samples, and assess communication before approving production. This guide compares leading manufacturers through capability, compliance awareness, customization, sustainability, and dependable delivery. Claims should be checked carefully, because attractive packaging does not automatically prove pharmaceutical reliability.
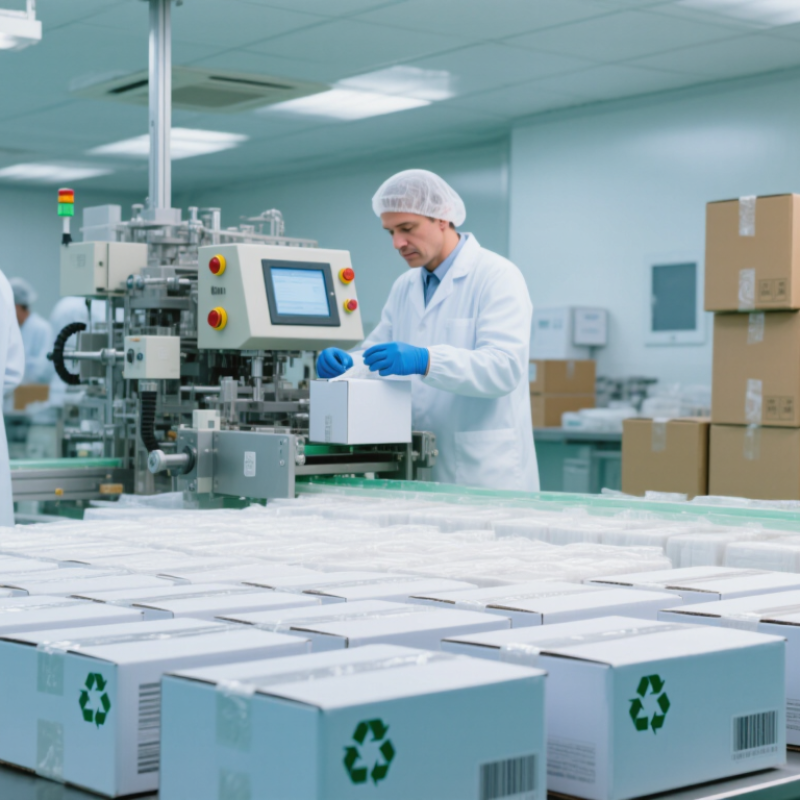
Top Custom Pharmaceutical Packaging Boxes Manufacturers?

What Defines a Top Custom Pharmaceutical Packaging Box Manufacturer?

A top custom pharmaceutical packaging box manufacturer is defined by controlled performance, not attractive artwork. Experience begins with understanding product sensitivity, filling equipment, storage conditions, and distribution risks.

The manufacturer should operate documented quality systems and follow GMP principles. ISO 15378 certification is also valuable for suppliers producing primary packaging materials for medicinal products.

Reliable manufacturers test paperboard strength, print accuracy, coating adhesion, moisture resistance, and dimensional fit. They should provide batch records, material certificates, inspection samples, and full traceability.

The World Health Organization reported that one in ten medical products in low- and middle-income countries is substandard or falsified. Packaging cannot solve every supply-chain problem. However, secure construction, controlled printing, and tamper-evident features can reduce avoidable risks.

A serious supplier also reviews artwork carefully. A missing warning or unclear dosage panel can create practical confusion. That detail is easy to underestimate.

Tips:

Request a pilot batch before large production. Check color consistency under standard lighting. Ask for test results, not general promises. Compare the approved sample with packed cartons. Small differences matter.

Sustainable materials should be assessed for barrier performance, not selected only for marketing. The Healthcare Packaging Market report by Smithers identifies sustainability, serialization, and automation as continuing industry priorities.

Still, no manufacturer gets every variable right. The strongest partner documents problems early, explains corrective action, and welcomes independent audits. Reliability is visible in the records, the samples, and the response when something goes wrong.

WHO’s 1-in-10 Falsified-Medicine Risk: Packaging Security Criteria

Top Custom Pharmaceutical Packaging Boxes Manufacturers?

WHO has reported that roughly one in ten medical products in some low- and middle-income markets may be falsified. Packaging cannot remove every risk. It can, however, make interference visible and verification easier. Reliable manufacturers should understand tamper-evident seals, serialized codes, secure substrates, and controlled artwork files. They should also provide documented testing, batch records, and traceable production data. Ask for evidence, not impressive claims.

A strong pharmaceutical box should show clear damage after opening. Tear strips, fragile seals, and locking features need practical testing. Serialization should connect each carton to approved production records. Hidden markers may support inspection, while visible codes help pharmacies and patients verify products. Material strength matters too. Weak folding cartons can split during transport, exposing labels or dosage information. Good suppliers review storage conditions, humidity, handling, and packing-line performance before recommending a structure. Custom printing alone is not security. A polished box can still be copied.

Tips: Request samples from multiple production batches. Test opening, scanning, stacking, and moisture exposure. Check whether codes remain readable after abrasion. Confirm who controls digital artwork and variable data. Use independent quality reviews when possible. Some security features sound excellent but fail in daily handling. That weakness deserves attention before approval.

ISO 15378:2017 and GMP: Auditing Custom Pharmaceutical Box Makers

Selecting top custom pharmaceutical packaging box manufacturers requires more than comparing prices or printed samples. ISO 15378:2017 and GMP should guide the audit. These standards connect packaging production with quality risk management and product protection. A certificate alone is not proof. Ask for its scope, expiry date, and certification body.

During an audit, inspect material receiving, artwork approval, printing, cutting, gluing, and final release. Check whether each paperboard batch has a supplier record and traceable lot number. Review color standards, barcode checks, dimensional measurements, and line-clearance procedures. Packaging should not carry mixed artwork or unidentified components. Small details matter.

Ask how the manufacturer controls dust, moisture, pests, and foreign materials. Review employee training records, equipment maintenance, deviation reports, and CAPA effectiveness. Change control deserves close attention. A minor ink, paper, or tooling change can affect readability and packaging performance. Request retained samples and batch records, then compare them with actual production.

Use a risk-based audit plan. Prioritize critical box features, especially tamper evidence, folding accuracy, print legibility, and transport durability. A site visit often reveals more than a polished presentation. Look at housekeeping. Observe operators. Ask them to explain a recent quality problem. Their answers may expose weak procedures.

No audit is perfect. Auditors can miss routine shortcuts. Follow-up evidence is essential. Some findings need deeper review, not quick acceptance. A reliable manufacturer welcomes difficult questions and provides clear, dated records. That behavior supports trust more than attractive packaging samples.

Top Custom Pharmaceutical Packaging Boxes Manufacturers? - ISO 15378:2017 and GMP: Auditing Custom Pharmaceutical Box Makers

Audit Dimension ISO 15378:2017 / GMP Expectation Evidence to Review Suggested Weight Audit Result
Quality Management System A documented, controlled quality system should cover pharmaceutical packaging-material activities, responsibilities, procedures, records, and continual improvement. Quality manual, approved procedures, organization chart, quality objectives, management-review records, and internal-audit reports. 15% Verify
Pharmaceutical GMP Controls Operations should be performed under controlled conditions that reduce risks of contamination, mix-ups, defects, and unintended changes to packaging components. GMP procedures, production instructions, hygiene rules, line-clearance records, pest-control records, and contamination-control measures. 15% Verify
Design and Artwork Control Specifications, approved artwork, print content, dimensions, and revisions should be reviewed and controlled before production. Master artwork, version history, approval records, color standards, customer specifications, and obsolete-artwork controls. 10% Verify
Supplier and Material Control Paperboard, inks, coatings, adhesives, and other inputs should be purchased from approved sources and evaluated against defined specifications. Approved-supplier list, incoming inspection records, certificates of analysis or conformity, material specifications, and supplier evaluations. 10% Verify
Production Process Validation Processes whose results cannot be fully verified by later inspection should be appropriately validated; critical printing, folding, gluing, and coding controls should be defined. Process-validation protocols and reports, equipment qualification, setup approvals, in-process inspection plans, and capability data where applicable. 15% Verify
Identification and Traceability Materials and finished packaging components should be identifiable throughout receipt, processing, storage, release, and distribution. Batch or lot numbers, job travelers, barcode or label controls, status identification, production records, and distribution records. 10% Verify
Inspection and Testing Inspection methods should be documented, suitable for the product, and supported by calibrated or verified measuring equipment. Sampling plans, inspection specifications, test methods, calibration certificates, defect classifications, and retained inspection records. 10% Verify
Nonconformity and CAPA Defective or nonconforming packaging should be identified, segregated, investigated, and dispositioned. Corrective and preventive actions should address root causes. Nonconformance reports, deviation investigations, root-cause analyses, CAPA plans, effectiveness checks, and rejection records. 10% Verify
Change Control Changes affecting materials, suppliers, equipment, artwork, processes, specifications, or testing should be assessed, approved, documented, and communicated. Change-control procedure, risk assessments, approval workflow, validation impact assessments, and customer notification records. 8% Verify
Document and Data Integrity Records should be legible, attributable, contemporaneous, original or verified copies, accurate, complete, and protected from unauthorized alteration. Document-control procedure, electronic-system access controls, audit trails where applicable, record-retention policy, and training records. 7% Verify
Total Suggested Audit Weight 100% Audit Required
Assessment note: ISO 15378:2017 applies specifically to quality-management systems for manufacturers of primary packaging materials for medicinal products. Packaging-box suppliers should also be assessed against the applicable customer specifications, regional pharmaceutical GMP requirements, and the intended use of the box.

EU FMD 2D Codes and U.S. DSCSA: Serialization Readiness

Top Custom Pharmaceutical Packaging Boxes Manufacturers?

EU FMD 2D Codes and U.S. DSCSA: Serialization Readiness

Choosing a custom pharmaceutical packaging box manufacturer now requires more than attractive artwork. The supplier must understand regulated serialization workflows. For EU markets, cartons commonly carry a GS1 DataMatrix code with product information, a unique serial number, batch details, and expiry date. The code must remain readable after folding, varnishing, transport, and warehouse handling.

U.S. DSCSA readiness requires package-level product identification and secure electronic data exchange. A capable manufacturer should support serial number generation, verification, aggregation, and controlled data records. Ask how printers manage rejected codes. Ask where inspection images are stored. These details reveal operational experience. A clean sample is not enough.

Physical packaging still matters. A box may include tamper-evident features, controlled colors, tactile marks, and a clear human-readable code beside the DataMatrix. Printing tests should use the final substrate, ink, coating, and packaging line speed. Small changes can affect contrast and scanning. This is where some projects fail quietly. The artwork passes approval, but the code becomes weak after finishing. Manufacturers should provide documented validation, calibrated vision checks, change control, and traceability for every production lot. No implementation is perfect at first. Pilot runs, independent verification, and realistic transport testing help expose mistakes before commercial release.

Top Custom Pharmaceutical Packaging Boxes Manufacturers? — EU FMD 2D Codes and U.S. DSCSA: Serialization Readiness

The timeline highlights major serialization milestones affecting pharmaceutical packaging. EU FMD safety features became mandatory on 9 February 2019, while U.S. DSCSA requirements progressed toward package-level, interoperable electronic tracing in 2023. FDA guidance provides a stabilization period for enhanced DSCSA requirements through 27 November 2026, making 2D-code printing, unique product identifiers, aggregation, verification, and data exchange important packaging-readiness considerations.

Sources: European Commission, Falsified Medicines Directive 2011/62/EU and Delegated Regulation (EU) 2016/161; U.S. FDA, Drug Supply Chain Security Act implementation resources and stabilization-period guidance.

Ranking Manufacturers by MOQ, Lead Time, Cost, and Defect-Rate Data

Top Custom Pharmaceutical Packaging Boxes Manufacturers?

Ranking Manufacturers by MOQ, Lead Time, Cost, and Defect-Rate Data

A reliable ranking starts with comparable factory data, not glossy samples. PMMI’s 2024 pharmaceutical-packaging industry report highlights automation, labor pressure, and supply continuity as major purchasing concerns. For custom boxes, record MOQ, approved artwork date, production days, and shipment variance. An MOQ below 5,000 boxes offers flexibility, but usually increases unit cost. Lead times of 20 to 35 business days are practical for standard folding cartons after artwork approval.

Cost needs deeper checking. Compare tooling, proofing, freight, inspection, and rework charges together. A supplier quoting 0.08 dollars less per box may become more expensive after rushed delivery. We made this mistake once. It looked efficient.

Defect-rate evidence deserves the highest score. Request three consecutive lot records, not a single inspection photo. A sensible screening benchmark is below 0.5% critical defects and below 1.5% total visual defects, although these are buyer benchmarks, not universal legal limits. FDA current good manufacturing practice guidance requires controlled procedures and documented inspections, supporting traceability during supplier evaluation. Rank manufacturers by verified performance: MOQ flexibility, median lead time, landed cost, and defect data. Missing records should reduce the score. Silence is data, too.

FAQS

Why does pharmaceutical packaging need security features?

Packaging can reveal interference and support product verification. It cannot remove every falsification risk. That limitation matters.

Which tamper-evident features are useful?

Tear strips, fragile seals, and locking structures can show visible damage after opening. Test them under realistic handling conditions. Appearance alone proves little.

What should a reliable packaging manufacturer provide?

Request documented testing, batch records, controlled artwork files, and traceable production data. Ask for evidence, not impressive claims. Samples are helpful.

How should serialized codes be managed?

Each carton should connect with approved production records. Suppliers should support code generation, verification, aggregation, and secure data exchange. Rejected codes need documented handling.

What can weaken a two-dimensional code?

Folding, varnish, abrasion, transport, and warehouse handling can reduce readability. Test the final substrate, ink, coating, and line speed. Small changes matter.

How can packaging materials protect products during transport?

Strong cartons resist splitting, moisture, stacking pressure, and repeated handling. Suppliers should review storage conditions before recommending a structure. Weak folds create problems.

What tests should buyers request before approval?

Test opening, scanning, stacking, abrasion, moisture exposure, and transport performance. Use samples from several production batches. One clean sample is insufficient.

How can artwork and variable data remain controlled?

Confirm who controls digital artwork, serial numbers, inspection images, and change approvals. Controlled access reduces accidental errors. Still, no process is flawless.

Why are pilot runs and independent reviews valuable?

Pilot runs can expose weak contrast, failed seals, and scanning problems before commercial release. Independent checks add useful pressure. Some mistakes remain hidden.

Conclusion

Top Custom Pharmaceutical Packaging Box Manufacturers are defined by their ability to combine product protection, regulatory awareness, reliable production, and consistent quality. Custom Pharmaceutical Packaging Boxes should protect medicines from moisture, light, contamination, and physical damage while supporting clear labeling and secure handling. Because falsified medicines remain a serious global concern, manufacturers should offer tamper-evident features, traceable materials, authentication options, and strong quality-control procedures.

A thorough evaluation should examine compliance with ISO 15378:2017 principles and GMP expectations, including documented processes, material controls, hygiene, testing, and audit readiness. Manufacturers should also demonstrate serialization readiness for 2D codes used under the EU FMD and U.S. DSCSA frameworks, with accurate printing, inspection, and data coordination capabilities. The final ranking can compare minimum order quantities, lead times, total cost, defect rates, production flexibility, and customer support. This balanced approach helps buyers select a dependable packaging partner based on measurable performance rather than appearance alone.
Amelia

Amelia

Amelia is a dedicated marketing professional with a strong understanding of the company’s products, services, and long-term vision. Through her experience in market research, content strategy, customer communication, and digital marketing, she helps transform complex product information into clear,......